

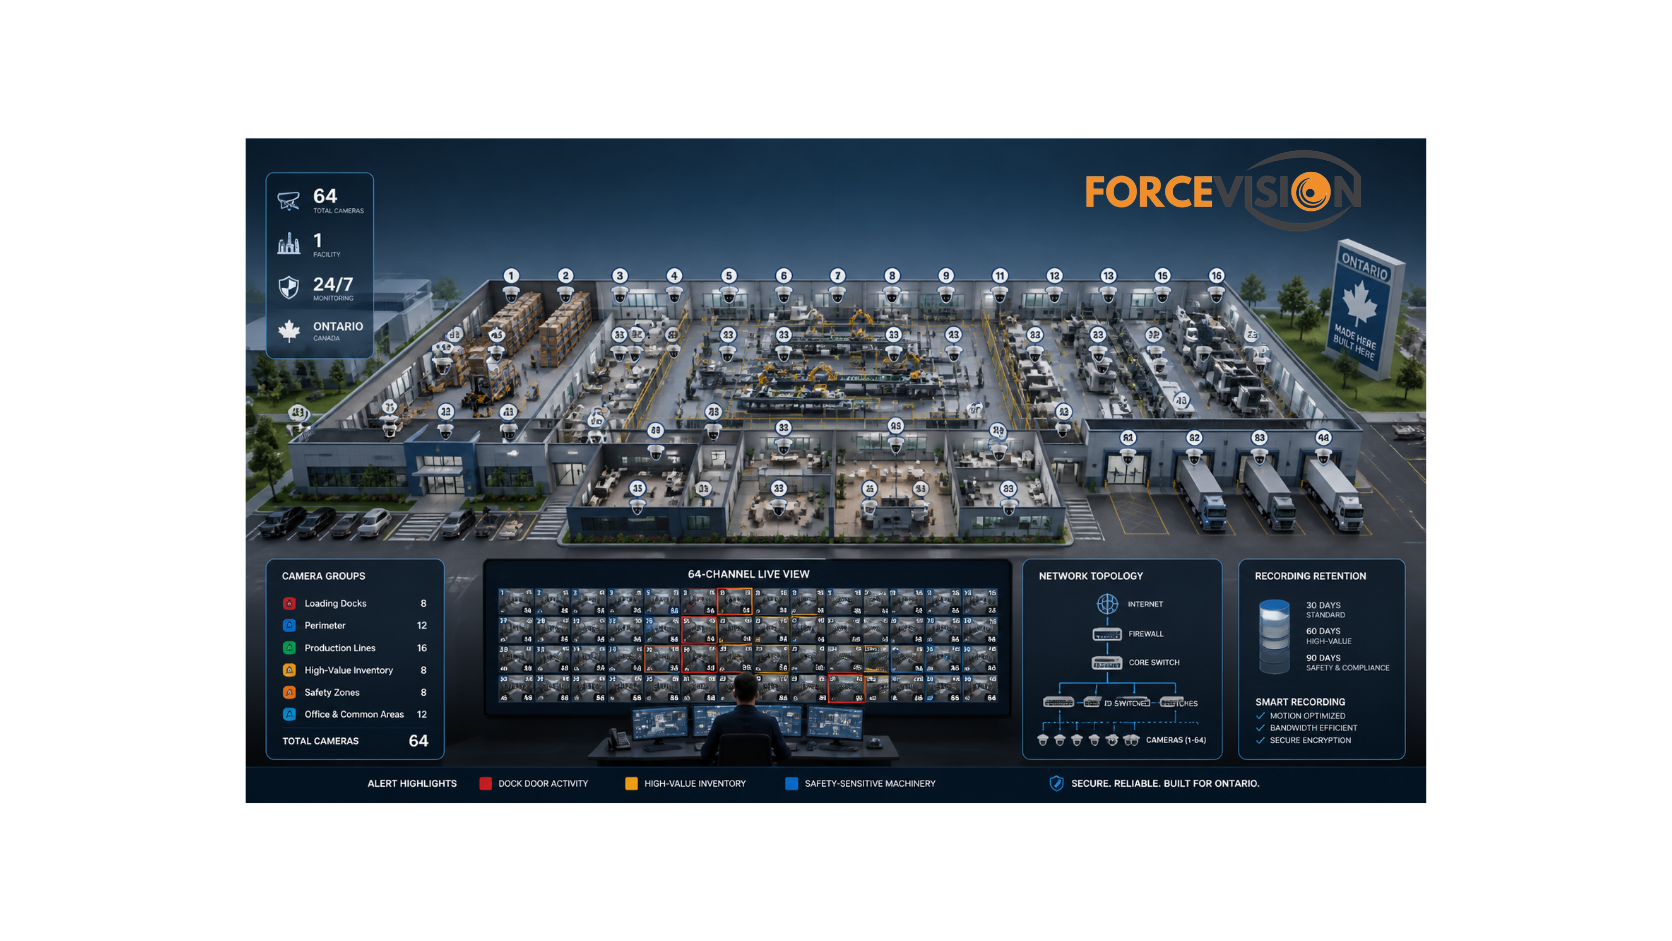
In large Ontario manufacturing plants, the production floor is only part of the risk picture. Raw material yards, finished goods warehouses, shipping docks, and staff parking lots all play a role in both loss and safety. When incidents occur — from internal theft to near‑miss injuries — many operations leaders discover their camera system simply doesn’t see enough. That’s where 64‑camera CCTV for Ontario manufacturing plants becomes the new normal.
This isn’t about making sites feel like surveillance states. It’s about giving security, operations, and safety teams a clear, shared view of what actually happens across a complex facility. As theft, fraud, and safety expectations grow, a well‑designed 64‑camera IP platform can help plants from Hamilton to Kitchener reduce shrink, respond to claims, and keep people safer without slowing production.
Where do manufacturers typically under‑cover with cameras?
Most legacy systems started small: a handful of cameras at main entrances, a view of the shipping dock, and maybe a monitor in the guard shack. As plants expanded, added lines, or built new warehouses, the camera count rarely kept up. Common blind spots include:
-
Exterior material yards where coils, pallets, or bulk inventory sit for days.
-
Secondary shipping doors used by specific customers or carriers.
-
Mezzanines, catwalks, and maintenance areas where falls or unsafe shortcuts can occur.
-
Staff and contractor parking lots where vehicle damage or theft complaints arise.
A 64‑camera CCTV for Ontario manufacturing plants allows operators to systematically cover these areas without having to choose between security, safety, and operational visibility.
How should a 64‑camera system be structured in a plant?
A practical design approach starts with mapping cameras to functional zones rather than simply sprinkling devices evenly. For example:
-
Perimeter and yard: Fixed bullet cameras along fence lines, loading bays, and gates to capture vehicles, visitors, and outdoor storage.
-
Shipping and receiving: Dome cameras over every active dock, with views of staging lanes, scales, and check‑in desks.
-
Production floors: Select cameras in high‑risk or high‑value areas (such as rework, scrap, or quality hold zones) rather than blanket coverage of every workstation.
-
Warehousing: Overhead views of aisles, pick faces, and pallet storage to monitor forklift behaviour and potential internal theft.
-
Common and parking areas: Coverage for entrances, lobbies, timeclock areas, and lots to support HR and safety teams.
With 64 cameras available, plants can avoid the constant trade‑off between “must have” and “nice to have” views, while still respecting privacy expectations through careful placement and policies.
How can analytics help manufacturing operations, not just security?
Modern NVR platforms and analytics engines can turn a 64‑camera CCTV for Ontario manufacturing plants into a multipurpose operational tool. Beyond detecting intrusions after hours, analytics can:
-
Monitor forklift and pedestrian interactions in shared zones, flagging repeated near‑misses.
-
Track congestion at docks or staging areas, helping planners adjust shift schedules or carrier appointments.
-
Detect blocked fire exits or emergency routes that become storage zones during peak periods.
-
Highlight unusual activity around high‑value components areas or tool cribs.
Used carefully, this data can inform layout changes, training priorities, and capital projects. The aim is not to “watch” workers more intensely, but to see patterns that traditional reporting misses.
What about privacy and workforce trust?
Any expansion to 64‑camera CCTV for Ontario manufacturing plants should include open communication with employees and unions where applicable. Clear signage, updated policies, and defined limits on how footage is used are essential.
Best practices include:
-
Documenting the primary purposes of CCTV (safety, security, quality, and incident investigation).
-
Restricting live viewing and playback to defined roles, with audit trails for access.
-
Setting retention periods that balance risk management with privacy considerations.
-
Training supervisors to avoid using CCTV as a “performance microscope” except in defined, policy‑aligned scenarios.
Handled well, employees often come to see cameras as a safety and protection tool — especially when footage helps resolve parking lot disputes, supports valid injury claims, or identifies hazards before someone is seriously hurt.
Integrating CCTV with access control, alarms, and MES
Manufacturing plants already juggle multiple systems: access control for doors, intrusion alarms, fire and life safety systems, and sometimes manufacturing execution systems (MES) or warehouse management systems (WMS). Integration is where 64‑camera CCTV for Ontario manufacturing plants moves from standalone to strategic:
-
Door alarms can automatically pull up corresponding camera views for security or supervisors.
-
Events such as after‑hours door openings or motion in restricted zones can trigger both alarms and video bookmarks.
-
Quality or scrap anomalies from MES can be cross‑checked against video near the affected line segment.
When designed as part of a broader plant technology stack, CCTV helps teams move faster and make stronger decisions based on shared visual evidence.
How ForceVision supports Ontario manufacturers
Every plant has its quirks: odd building additions, dark corners, critical lines, union rules, and legacy systems. ForceVision works with manufacturing and warehousing operations across Southern Ontario to design 64‑camera CCTV for Ontario manufacturing plants that respect those realities.
From Burlington and Hamilton steel and fabrication shops, through Kitchener‑Waterloo technology manufacturers, to large distribution‑heavy facilities around Brampton and Vaughan, ForceVision helps map risk zones, select the right mix of bullet, dome, and PTZ cameras, and design NVR platforms that scale. If you’re ready to move beyond a patchwork of legacy cameras, a no‑pressure assessment can clarify what a 64‑camera baseline looks like for your site.
Practical first steps for plant leaders
If you’re responsible for security, operations, or EHS at a large Ontario plant, consider:
-
Printing a current site plan and marking every existing camera and blind spot.
-
Listing recurring issues where video would help: internal loss, injuries, congestion, or customer disputes.
-
Engaging IT early to align on network, storage, and cybersecurity for a consolidated platform.
-
Updating your CCTV policy in parallel with any expansion, so expectations are clear.
64 cameras might sound like a lot — until you start mapping what truly matters across your plant.
FAQ
Q1: Do all 64 cameras need to be installed at once?
Not necessarily. Many plants phase deployments by zone, starting with the highest‑risk areas and expanding as budgets and priorities allow, provided the design anticipates full scale.
Q2: How much storage is needed for 64 cameras?
Requirements depend on resolution, frame rate, and retention period, but it’s common for large plants to provision several dozen terabytes of NVR or NAS storage to comfortably hold 30–90 days.
Q3: Can existing analogue cameras be reused?
Often, yes. Hybrid encoders and NVRs can integrate legacy analogue feeds while new IP cameras are added, helping manage budget and minimize disruption.
Q4: Who should own the CCTV program — security, operations, or IT?
The most successful programs treat CCTV as a shared asset, with clear governance across security or facilities, operations, safety, and IT. Each group has a stake in how the system is designed and used.


